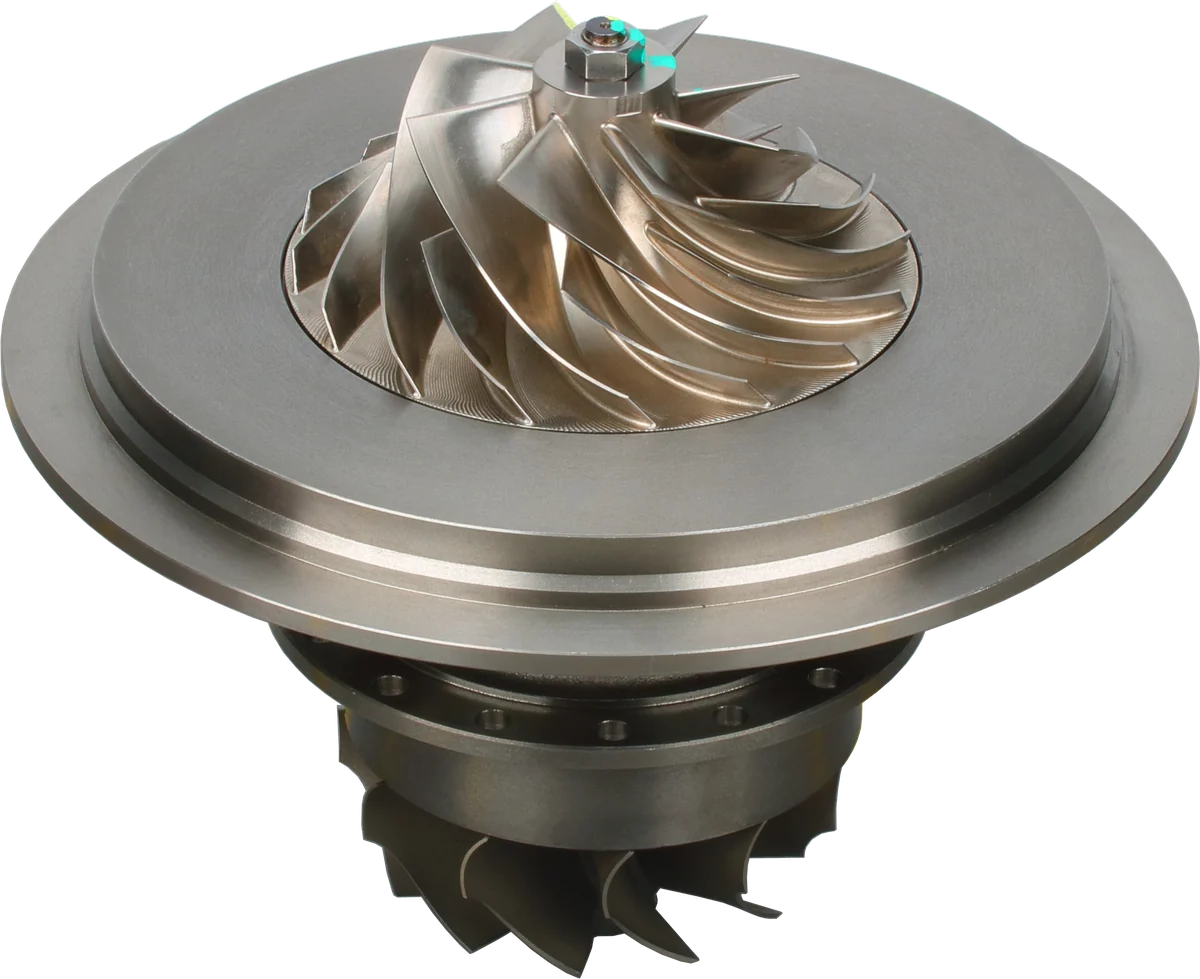
On a highway tractor, excavator, marine diesel, or generator set, rebuild quality depends on the parts accepted at the bench. New bearings cannot restore a worn housing bore, and a clean casting can still be cracked. Diesel turbocharger inspection before rebuilding establishes that every retained component has acceptable geometry, surface condition, and structural integrity.
Make that decision before ordering individual replacement parts. Several rejected components may change whether rebuilding the original assembly makes economic sense.
How should a turbocharger inspection checklist guide the job?
Identify the turbocharger by its full assembly number and revision. Engine identification alone may leave several possible wheel and bearing combinations. Get the applicable OEM service information, including reuse limits, inspection locations, and permitted repairs. A manufacturing dimension for a new part is not automatically the service rejection limit.
Before cleaning:
- Photograph deposits, contact patterns, and damaged areas.
- Record component identification and keep parts from different assemblies separated.
- Note whether damage appears concentrated at one bearing, wheel, or sealing interface.
- Preserve enough evidence to investigate the original failure.
Then clean using a process compatible with the component material and finish. Abrasive cleaning can alter dimensions or leave contamination in oil passages.
Measure clean parts at a stable temperature with checked turbocharger inspection tools. Record actual readings and the applicable acceptance criteria. If a required limit or repair method is unavailable, put the component on hold until that information is obtained.
How to inspect a used turbocharger
This table organizes the bench inspection; it does not establish universal turbo reuse limits. A reuse candidate must pass every applicable check, including checks on its mating components.
| Part | What to check | Tool | Typical action |
|---|---|---|---|
| Center housing | Blocked oil passages, corrosion, cracks, bearing-bore wear | Inspection light, suitable bore gauge | Clean and verify passages; reject unacceptable bore or casting damage |
| Shaft journals | Diameter, taper, ovality, scoring, surface finish | Outside micrometer, surface-finish instrument | Retain only within specified dimensional and finish limits |
| Shaft sealing grooves and threads | Worn groove walls, damaged lands, chipped or stretched threads | Magnification, groove and thread gauges | Replace when sealing or fastening geometry is unacceptable |
| Turbine shaft/wheel assembly | Straightness and runout | Dial indicator with V-blocks or specified fixture | Verify setup; reject excessive runout |
| Turbine wheel and shaft joint | Blade damage, oxidation, erosion, weld-area cracks | Magnification, approved crack-detection method | Reject cracked, distorted, or excessively deteriorated assemblies |
| Compressor wheel | Bore galling, nut-seat damage, blade and hub cracks | Magnification, suitable bore gauge, approved penetrant inspection | Replace damaged wheels |
| Thrust collar and flinger | Scored faces, worn bore, damaged sealing grooves | Micrometer, bore and groove gauges | Replace worn or damaged components |
| Journal bearings | Scoring, blocked oil holes, bore and outside-diameter wear | Magnification, micrometer, suitable bore gauge | Document wear pattern; renew for a full rebuild |
| Thrust bearing | Working-face condition, oil grooves, remaining thickness | Magnification, micrometer | Document wear; renew for a full rebuild |
| Backplate | Cracks, corrosion, seal-bore wear, seating-face damage | Magnification, bore gauge, specified flatness check | Reuse only when all relevant features pass |
| Heat shield | Distortion, cracks, interference, damaged seating | Visual inspection, reference surface or specified fixture | Replace if damaged or unable to seat correctly |
| Compressor and turbine housings | Wheel-contour damage, rub marks, cracks, erosion | Lighting, magnification, specified contour checks | Approved cleanup where permitted; otherwise replace |
| Flanges and mounting interfaces | Warping, pitting, damaged registers or threads | Straightedge, gauges, approved fixture | Repair only by an approved method or replace |
Do not approve components independently of their fits. An acceptable shaft diameter and an acceptable bearing bore must still produce the specified assembled clearance.
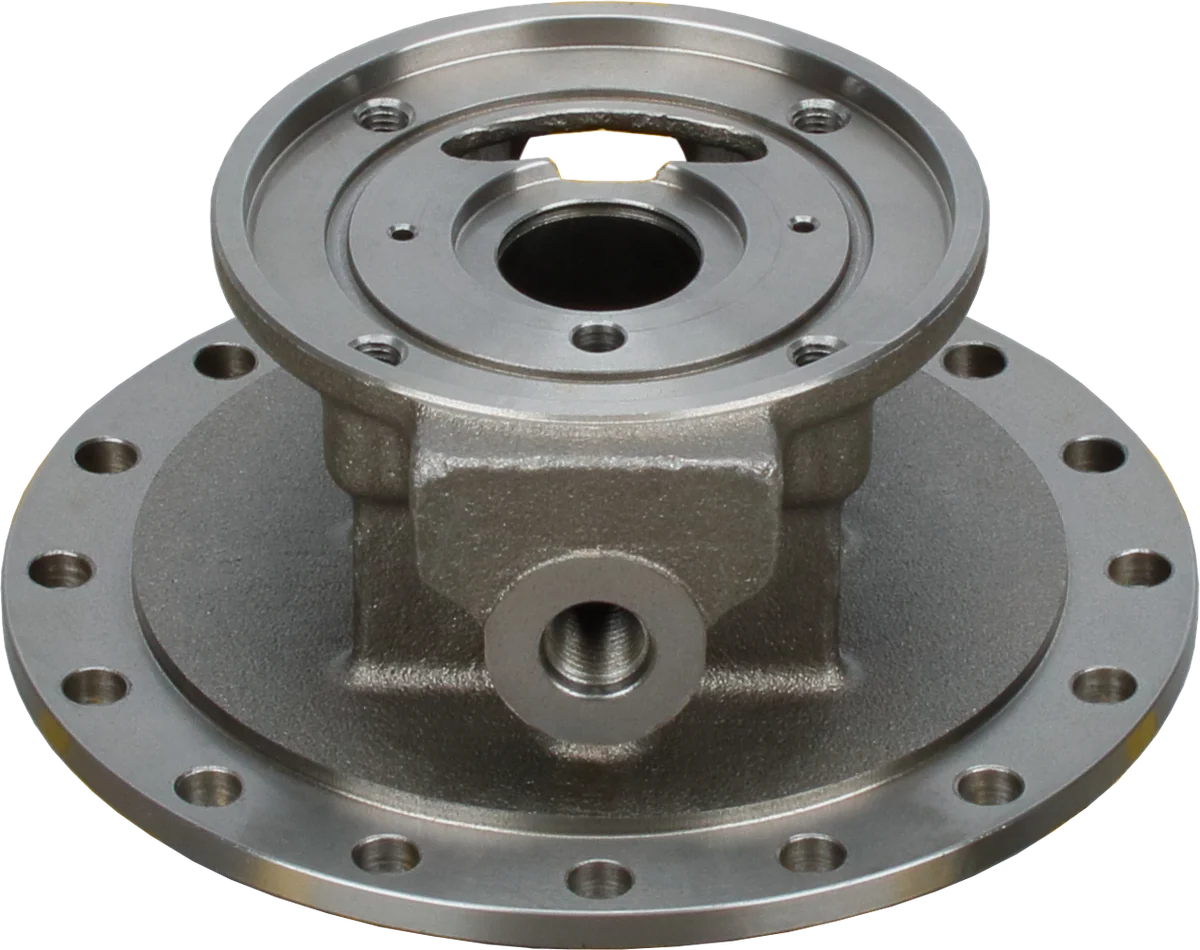
Central bore: houses the shaft and bearing system.
Mating surface: check cleanliness and damage.
Product photograph from 2026. Numbers identify the features explained below.
Measure geometry before deciding a shaft is reusable
Measure shaft journals at multiple positions along their working length and in different directions. A single reading can miss taper or ovality. Keep measurements associated with their locations so another technician can review the decision.
Apply the same approach to housing bores. Check the prescribed depths and directions, using a gauge suitable for the bore size and access. Do not average a failed measurement into an acceptable result.
| Instrument | Useful check | What prevents a false pass |
|---|---|---|
| Outside micrometer | Shaft diameter, collar dimensions, thrust-bearing thickness | Measure the specified surfaces at several positions |
| Bore gauge | Housing bores, bearing bores, component fits | Set against a suitable reference and check different directions |
| Dial indicator on V-blocks | Shaft runout at specified locations | Use the required support surfaces and a clean, stable setup |
| Surface-finish instrument | Journal and thrust-face texture | Compare the correct finish parameter with the OEM requirement |
A surface that looks shiny may still have unsuitable roughness or directional scoring. A finish comparator can assist screening, but use the specified measurement method when finish determines acceptance.
For runout, support the shaft as instructed and rotate it slowly while observing the indicator. Record total indicator reading at the required locations. Burrs, dirt, worn support journals, or an unsuitable fixture can distort the result, so verify questionable readings.
Shaft bend matters because the rotating assembly no longer follows its intended geometry. It can compromise running clearance and bearing behavior. Removing material during balancing cannot restore a bent centerline. Establish acceptable straightness before balancing.
Inspect surfaces and screen for cracks
For the center housing rotating assembly, or CHRA, dimensional checks and crack inspection answer different questions. A component can measure correctly while containing a flaw that rules out reuse.
Under strong lighting and magnification, examine these areas:
- Turbine shaft and wheel: Check blade roots, tips, rear surfaces, and the wheel-to-shaft joint. Look for cracking, deformation, missing material, and oxidation or scaling that has reduced the metal section.
- Compressor wheel: Inspect both blade faces, the hub, bore, and nut seat. Galling can interfere with correct fit, while fretting or an uneven seat can compromise clamping. Reject cracked or distorted blades.
- Thrust collar and flinger: Check working faces, shaft fits, and sealing grooves. Grooving, heat distress, or damaged groove sidewalls can make the component unsuitable despite an acceptable outside appearance.
- Shaft threads: Inspect the full engaged length. Confirm the correct thread specification and direction. Do not use a new nut to force damaged threads into apparent usability.
Dye penetrant can reveal cracks that open to the surface. Use a procedure approved for the component and material, with a clean, dry surface and the specified application, removal, and development steps. Rough surfaces and retained contamination can complicate interpretation.
A clear penetrant result does not establish freedom from internal defects. Have uncertain indications evaluated through a qualified inspection process. A confirmed crack in a wheel, shaft, or shaft joint is a rejection condition.
Do not straighten blades or grind away a crack to make a rotating part appear serviceable.
Turbocharger housing reuse vs replacement
A rub mark needs assessment beyond its appearance. Determine whether the mark is transferred wheel material, a shallow surface disturbance, or actual loss of housing material. Inspect the corresponding wheel and investigate why contact occurred.
Light marks may be eligible for an approved cleanup when the finished housing retains its specified contour and wheel clearance. Removing a raised deposit is fundamentally different from cutting away sound material to erase a groove.
Replacement is generally appropriate when damage leaves an enlarged or distorted contour, compromises structural integrity, or cannot be evaluated against an approved repair criterion. Do not grind broadly around a local rub just to make the surface look uniform.
Also inspect flange faces, clamp lands, mounting registers, and threaded holes. Pitting or distortion can prevent correct sealing and alignment. Machine a flange only when the approved repair procedure permits it.
Inside the center housing, verify the complete oil path. Clear inlet and drain openings do not prove that every bearing-feed drilling is clear. Check for retained debris and cleaning residue before approving the casting.
Which turbocharger parts need replacing?
Treat removed seal rings, nuts, locks, O-rings, bolts, snap rings, and gaskets as consumables and replace them during the rebuild. Order by the exact turbo specification.
| Consumable | Why replacement matters | Verify before assembly |
|---|---|---|
| Metal sealing rings | Used contact surfaces and ring condition affect sealing | Correct ring design and compatible groove |
| O-rings and gaskets | Disturbed or aged seals may not reseal reliably | Correct material, profile, and application |
| Nuts, bolts, and locks | Retention depends on correct fastening hardware | Thread, grade, length, and locking arrangement |
| Snap rings | Removal or damage can compromise retention | Correct section, groove fit, and seating |
For a full rebuild, renew journal bearings and the thrust bearing as well. Inspect the removed bearings first: scoring, uneven wear, and blocked oil features help identify damage elsewhere in the assembly.
Measure old thrust-bearing thickness between its working faces at several suitable positions. Uneven thickness or wiped working surfaces should prompt close inspection of the mating collar. Installing a new bearing against a damaged collar leaves part of the wear problem in place.
Inspect backplate sealing bores and ring grooves just as carefully. Fresh sealing parts cannot compensate for worn mating geometry.
Close the inspection record before balancing
Complete the turbocharger inspection checklist with a disposition for each component: accepted, replaced, held for further evaluation, or repaired under an approved process.
The record should include:
- Component identification and measured results.
- The service criteria used for acceptance.
- Crack-inspection findings and any authorized repair.
- Replacement-part specifications and required assembly checks.
CHRA inspection is complete only when the retained components and their combined fits are acceptable. Follow the required balancing and final verification process afterward. Free rotation by hand is useful during assembly, but it does not establish correct operating clearance, balance, or sealing performance.
Parts for this guide
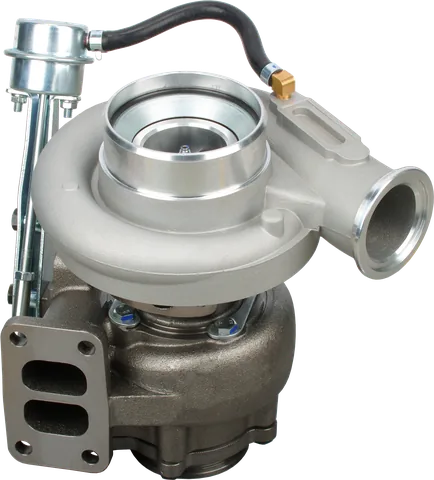
 GTB1649V Turbocharger Core 757886-0003 | Kia Sportage II 2.0 CRDI
FOR 757886-0003
Core
On backorder — orders accepted
 4027045 HX50W Turbocharger Repair Kit for Weichai WP10
4027045
Repair kit
On backorder — orders accepted
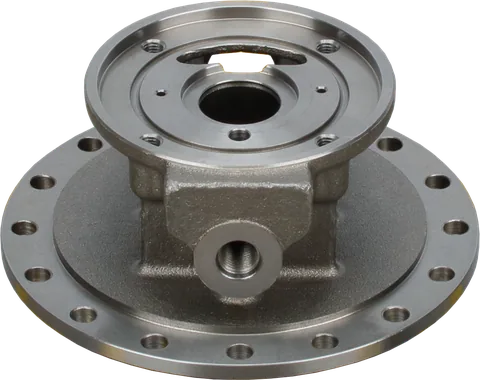
 3533983 HX60 Turbocharger Bearing Housing for Scania DSI14-44
3533983
Bearing housing
In Stock
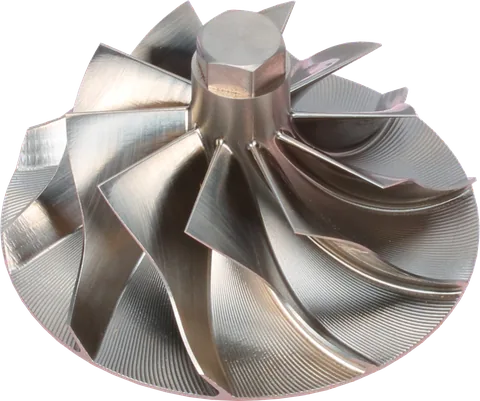
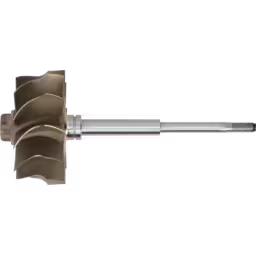 3522064 TW H2C Turbine Wheel for Cummins M11 & Volvo TD123E
FOR 3522064 TW
Turbine wheel
In Stock
Common Questions
Can a turbine shaft be reused after polishing?
Only if an approved process removes superficial marks while preserving the required diameter, geometry, and finish. Polishing cannot make an undersize journal acceptable. Recheck dimensions and surface condition before considering the assembly for reuse.
Does balancing correct a bent shaft?
No. Balancing corrects uneven mass distribution; it cannot restore the centerline of a bent shaft. Measure runout before balancing and reject a shaft that exceeds the applicable limit.
Can a housing with light rub marks be reused?
Sometimes, if an approved cleanup preserves the specified contour and wheel clearance. Deep grooves, distortion, and structural damage usually rule out that approach. Inspect the mating wheel and correct the cause of contact before reusing the housing.
When should a shop choose a replacement CHRA?
Consider a correctly matched, balanced CHRA when rotor damage, worn center housing bores, or missing inspection data prevent a defensible rebuild. The existing housings still need inspection, and the original failure cause must be corrected.
Can a turbocharger inspection checklist replace OEM limits?
No. It organizes the work, but acceptance depends on the exact turbocharger model, its service data, and any approved repair process. If a required limit is unavailable, do not assume that an apparently clean part is reusable.
What are signs of worn turbocharger parts?
Look for scoring, uneven wear, worn bores, and damaged grooves. Evaluate each against the applicable reuse criteria.
Contact LeadTurbo with the turbo part number, engine details, and inspection findings for help identifying replacement turbochargers, CHRAs, repair kits, or individual parts.